

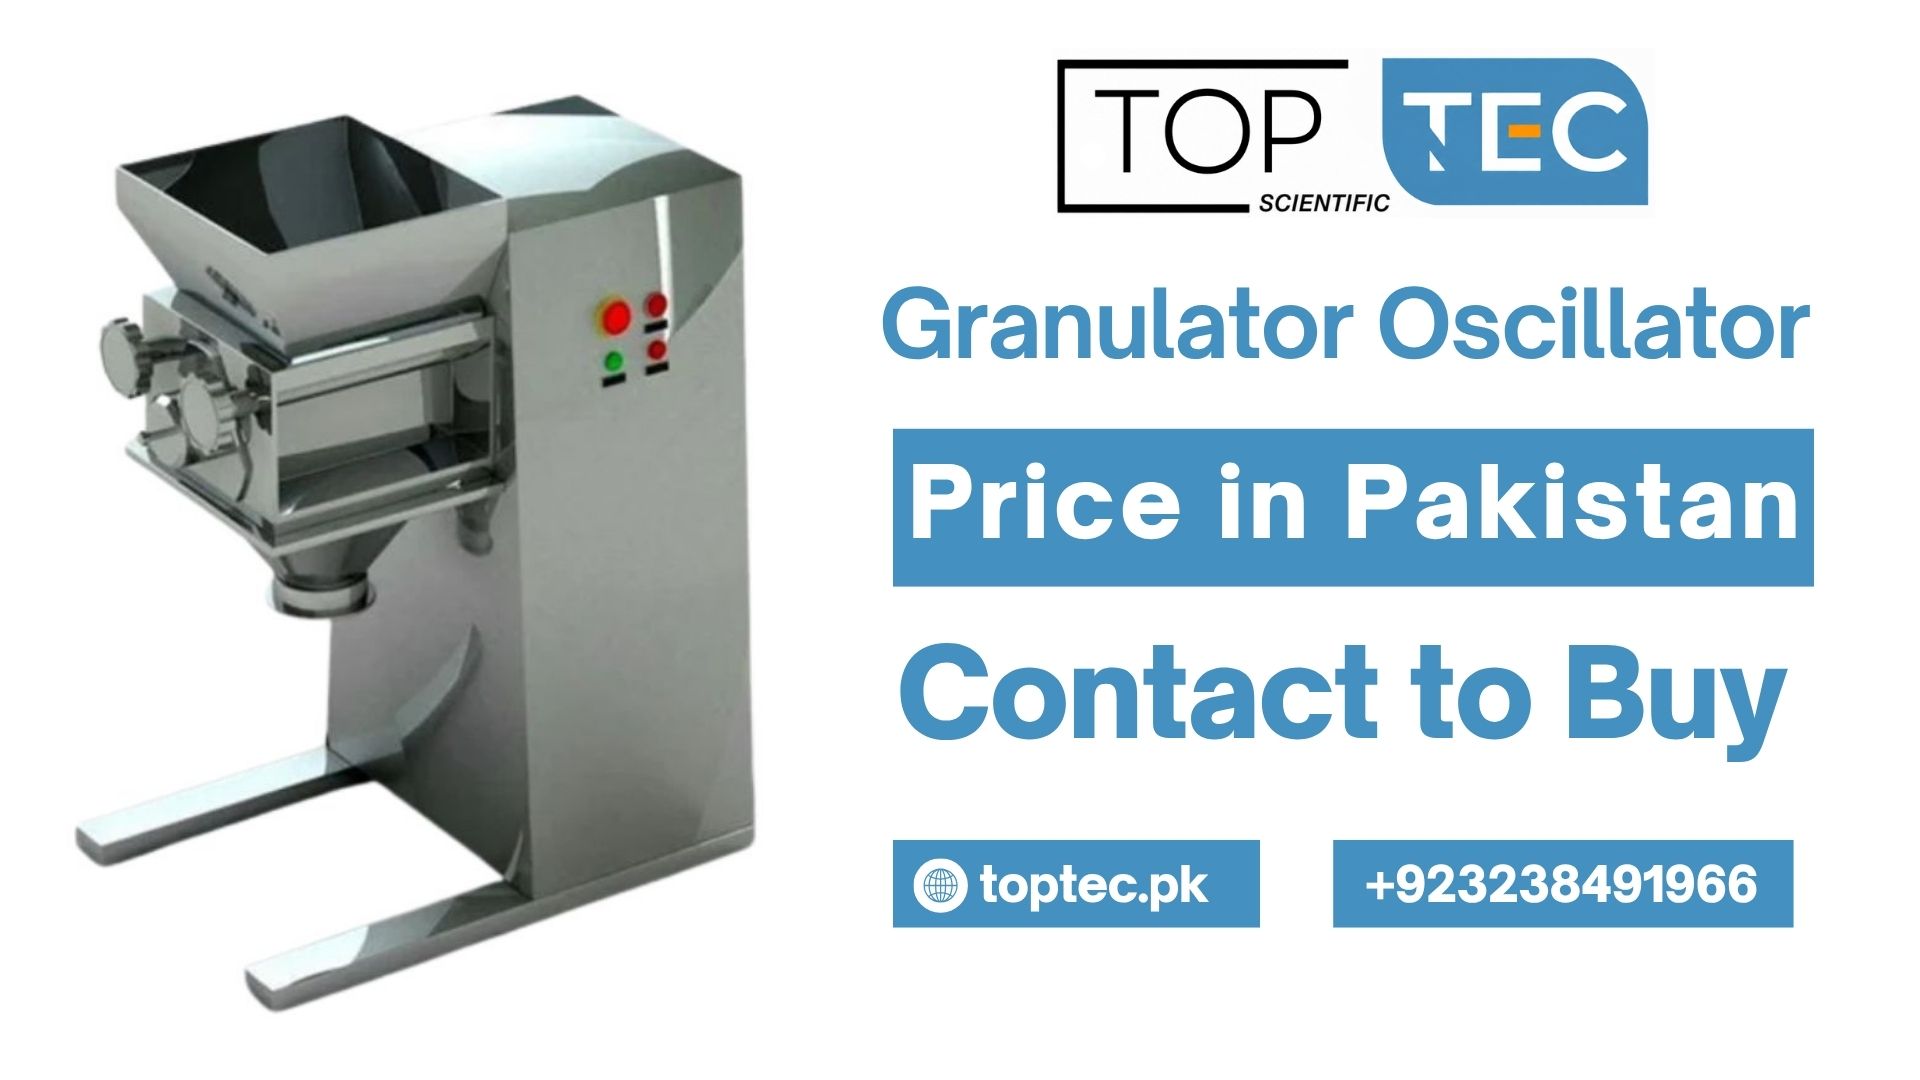
Learn how a Granulator Oscillator works. Understand the rotor, screen, and oscillation principles for pharmaceutical and chemical processing.
A buyer once called me after purchasing a machine that was sold to him as “200 kg per hour”. On paper, perfect. In his unit, with his actual product and a finer screen, he was getting somewhere around 60 to 70 kg on a good hour. On a bad day? Less. He was not cheated in the dramatic, filmi sense. Nobody had run away with his money. The spec sheet was just… technically true, under conditions that had nothing to do with his work.
That is the problem with specifications.
Almost every granulator oscillator machine looks great on a brochure. Shiny photos. Neat table. Confident numbers. But three specs decide whether you will be happy six months later — capacity, speed, and contact parts. Get those three wrong and the machine will remind you about it every single batch.
So let’s go through them the way I explain it on the phone when someone asks me, “Sir, ye model theek rahega?” Not textbook style. Practical style.
First, what is this machine even doing?
Very simple. You load damp mass in the hopper. Inside, a rotor keeps moving back and forth — oscillating, not spinning in full circles — and pushes that mass through a screen around the drum. Whatever passes through comes out as granules.
That’s it.
But, and this matters, the final granule is decided by small things. Screen a little too fine? Output drops. Mass a little too wet? Screen blinds. Rotor a bit too aggressive? You get fines, dust, and then your tablet compression starts acting strange two steps later.
People think granulation is a rough, forgiving step. It is not. It is quietly fussy.
The spec sheet most people get on WhatsApp
In Pakistan, half the buying process now happens on WhatsApp. Someone sends a photo of the machine. Then a PDF. Sometimes just a forwarded table with no model number.
For reference, this is roughly what I see for common sizes here. Do not treat this as a law. Every maker rates things differently, and some rate them very… optimistically.
| What you’re looking at | Small / lab type | Pilot type | Bigger production type |
|---|---|---|---|
| What sellers claim per hour | 5–30 kg | 30–100 kg | 100–300 kg, sometimes more |
| Hopper size | Around 5–10 litres | 15–30 litres | 35–60 litres |
| Oscillations in a minute | 120–180 or so | 120–180 or so | 110–170 or so |
| Motor | 0.5 to 1 HP | 1 to 2 HP | 2 to 5 HP |
| Mesh you’ll commonly use | 10 to 60 | 8 to 60 | 8 to 50 |
| Power you’ll need | 220V single-phase, usually | Single or 3-phase | Almost always 415V, 3-phase, 50Hz |
Seen this kind of table before? I’m sure you have.
The bit people miss is at the bottom. As machines get bigger, it is not only the hopper that gets bigger. The motor, the frame, the wiring, the power requirement — everything changes. I have actually seen a good machine delivered to a perfectly decent building where there was no proper three-phase point near the room it was meant for. Extension board se kaam nahi chalta, let me put it that way. The machine sat there for days while electricians argued in the corridor. Expensive embarrassment, totally avoidable.
Capacity. Ah, the famous number.
If there is one spec that causes the most arguments later, it is capacity.
When a seller says a granulator oscillator machine will do 200 kg per hour, my first reaction is not “wah”. My first reaction is: with what?
With what material? At what moisture? Through which mesh?
Because capacity is not a fixed property like the height of a table. It changes. A lot.
Lactose behaves one way. MCC behaves another. A sticky, haldi-coloured herbal mix that wants to stick to everything it touches? That is a completely different day at work. Wet mass is heavy and slow. Dry sizing moves faster but throws more dust. And the screen — please pay attention to this — the screen changes everything. Go finer and your throughput will fall. Every time. No exceptions because a brochure says otherwise.
Then there is feeding. Some operators dump the whole lot in, as if the machine is a bucket. It is not a bucket. Feed it steadily and the same machine suddenly seems better behaved. I don’t fully blame operators for this. Nobody tells them. The supplier sold “200 kg per hour”, so they expect 200 kg whether they feed it gently or throw it in like they are angry at it.
So here is my small, boring, very useful advice. When someone quotes capacity, ask one question: “Bhai, ye output kis mesh par test kiya tha?”
If he answers clearly, good. If he starts saying “sir, bus output zabardast hai, tension na lein”, write that down mentally. That is not an answer.
What size should you actually buy?
For lab and formulation work, smaller is usually smarter. Less wastage, faster cleaning, and you can try three variations in a day without hating your life.
Pilot size? Look at your batch, not the brochure. If you mostly make 20, 25, 30 kg batches, does the machine finish that in a sensible time without heating up or the screen choking? That is your answer. Not “100 kg per hour”.
Production is where people panic and buy too big. I understand why. They think future expansion, future orders, future everything. Sometimes they are right. Sometimes they end up cleaning a large machine for a medium batch every day, losing product inside it, and maintenance also costs more.
Buy for the batch you run every week. Not the imaginary batch you hope to run in 2028. Harsh? Maybe. But I have seen more money wasted on oversized equipment than on slightly undersized equipment. There. I said it.
Speed — not fast, not slow, just wrong can ruin it
Now speed.
On this machine you will mostly see OPM. Oscillations per minute. How many times the rotor swings back and forth in one minute. Commonly somewhere around 110 to 180. You will see variations. That is normal.
Too slow and the mass just sits there, smearing, passing unevenly. The process takes longer and granules do not look the same from start to end.
Too fast and the machine stops being gentle. It starts forcing. On a pharmaceutical granulator, that forcing shows up as fines, a bit of heat, and granules that looked okay in the tray but do not compress the way you wanted. Then everyone blames the tablet press. Sometimes the tablet press is innocent. Poor thing.
This is why I personally like variable speed, a VFD, if you run more than one product. If you have one fixed formulation and you have already standardised it, fixed speed can work. But if your work keeps changing — and in most small units it keeps changing — being able to slow down or speed up slightly is gold.
When you go see a machine, do not just switch it on and say “chal raha hai”. Ask them to change the speed slowly. Listen. Watch the rotor. Does it jerk? Does it surge? Does the display show 140 and the movement looks like something else entirely?
And do not talk over the machine while it is running. I know this sounds funny. Let it run. Machines talk, in their own way. A steady hum is one thing. A knocking that comes every few seconds is another. It is trying to tell you something before you pay. Listen now, or pay later. Your choice.
Motor size is usually somewhere from 0.5 HP in a small granulator oscillator machine up to 5 HP or more in larger ones. Bigger motor does not automatically mean better machine. It has to match the drum and the load. A weak motor sweats under load. You will see it getting hot, you will hear it struggling. In Pakistan summers, especially in a room with poor ventilation, this gets worse fast. Forty-five degrees outside, machines and humans both suffer. Keep that in mind.
Oh, and check the belt and the gearbox oil while you are there. Glazed belt, oil weeping from a seal, a pulley wearing on one side — small observations. Two minutes. They tell you a lot about the previous life of the machine. Or its future, if it is new and badly assembled.
Contact parts. This is where I become a bit stubborn.
Capacity gets people excited. Speed gets technical people excited. Contact parts? That is where I spend my time. Because this is what touches your product.
Contact parts in a granulator oscillator machine normally mean hopper, rotor, drum, screen, outlet chute, and those gaskets and seals sitting around them. If these are wrong, you can have the best motor in the world. It will not save you.
For pharma work, the expectation on product contact side is SS 316L. Outer body, frame, covers — SS 304 there is usually fine. Do not mix the two up and do not just accept “steel hai sir, imported hai”. Ask for the certificate. Yes, even if it feels awkward. The awkwardness lasts 20 seconds. A validation problem lasts much longer.
I always run my hand inside the hopper. Always. You are feeling for rough welds, sharp edges, pitting, places where powder will sit and refuse to leave during cleaning. A finish around Ra 0.8 micron or better is what people usually look for on contact surfaces, but my point is simpler: it should feel smooth, even, properly finished. Not like someone welded it on a Friday evening and wanted to go home.
One badly finished weld can become the star of your cleaning validation. And not in a good way. Your QA will find it, the auditor may find it, then everyone is standing around one corner inside one hopper discussing one weld. I wish I was exaggerating.
The screen is doing more work than people give it credit for
People treat the screen as an accessory. It is not an accessory. It is practically the decision-maker for your particle size.
Check mesh. Check tension. Check how it fits. Take it towards light and look. Small holes, stretched patches, a little tear near the edge — easy to miss in a dim godown, very easy to regret in production.
And ask about spares before you need them. If this exact mesh tears six months later, who in Pakistan will give it to you and in how many days? A machine waiting for a screen is just furniture. Heavy, expensive furniture sitting in the middle of your room making everyone feel guilty.
Same thing with the rotor and outlet. Does the material fall cleanly or does it hug corners? Are the gaskets proper pharma-grade silicone or something that has gone hard like old rubber? Powder is sneaky. Give it a tiny gap near the drive and it will find that gap. Then a cleaning issue quietly becomes a mechanical issue also. Two problems for the price of one. Not a good deal.
Last thing here. And I feel strongly about this one, maybe because I have suffered through it: can a normal person open the contact parts for cleaning without special tools and without calling three strong men from the store?
If dismantling takes half a day, you will pay that half day again and again. Every changeover. Every cleaning. Ask them to open it in front of you. It takes five minutes. If they keep saying “sir, bohat easy hai” but do not show you, well. You have your answer, in a way.
The unglamorous specs nobody puts in big font
This is the section people skip. Then they call back.
Power. Read the nameplate. I am serious, take a photo of the nameplate with your phone. Voltage, phase, HP, amps. In our setup it is usually 220V single-phase for small units and 415V three-phase, 50Hz for bigger ones. In many industrial areas, voltage fluctuation is a real thing. Summer, load, old wiring — you know the story. Ask your electrician what protection you need. Do not discover it after the motor complains.
Safety is not a “feature”. Emergency stop must stop the machine, fully, and it must stay stopped until someone restarts it properly. Interlock must mean something. If the machine happily runs with the guard open, or someone has made a clever little jugaar with wire to bypass it, I would walk away. I would not negotiate. I would walk away. In a GMP environment it is not only dangerous, it is indefensible.
Controls also matter. Old PLC, old timer, old speed controller — fine today, dead tomorrow, spare available nowhere. I have seen a healthy pharmaceutical granulator stand idle not because anything was wrong with granulation at all, but because one small controller failed and the exact spare had to be hunted like a rare bird. That is a stupid way for a good machine to die. Check it before.
And DRAP. If you are in pharma manufacturing in Pakistan, your site qualification matters. IQ, OQ, PQ — whatever is applicable at your site, plan it with QA from the start. Old papers from a previous owner help a little. They tell a story. They do not qualify the machine in your room, on your floor, on your electricity, with your SOP. Bring QA in early. They are not there to make your life difficult, even if it feels that way on some days. They see what buyers, excited by price, do not see.
When the machine is second-hand, the spec sheet is only half the truth
I have nothing against second-hand. Actually, for a lot of units, I think it is the sensible route. New is not automatically wise if the budget dies in the process.
But with a used granulator oscillator, you have to read the specs differently. Nameplate says one output, but the screen is tired, belt is loose, motor has seen better days — real output will be something else. Steel is written 316L somewhere, but who repaired what, and when? Nobody wrote it down. That does not mean reject it. It means verify it yourself.
Run your own material. If you cannot, run lactose or MCC. Not perfect, but it will expose mechanical problems. Watch for blinding. Time it properly, not roughly on your phone while also drinking chai. Check fines. Listen at minute one and then again at minute fifteen. Machines reveal themselves after they warm up. So do sellers, by the way.
And if it is a used granulator oscillator that someone says is “fully refurbished”, ask for the list. What was changed? Bearings? Seals? Belt? Screen? Was it tested under load or just switched on and declared healthy? Paint is not refurbishment. New paint over old problems is just… old problems, in a nicer colour.
Payment in stages helps. Some now, some after installation and a proper test, balance after documents. A seller who becomes angry at reasonable conditions is giving you information. Listen to that too.
The room around it — people forget this, then suffer daily
A granulator does not live alone. There is weighing before it, transfer after it, wet mass, screens, cleaned parts, wet trays, people moving around with material. If the room is badly planned, your machine may be fine and your process will still be painful.
That is why a lot of units Buy Laboratory Furniture at the same time when they set up this area. It sounds unrelated to granulation. It is not. Stainless or chemical-resistant surfaces clean better than laminate that starts swelling and peeling. Sealed cabinets keep powder out of places powder has no business going. A trolley for screens looks like a luxury until someone carries a screen across the room and damages its edge.
TOPTEC Scientific, for context, is based in Pakistan and manufactures these items here in Pakistan. That local bit matters more than people think at the buying stage. If your room is not a standard imported size — and most rooms in older buildings in Pakistan are not standard anything — local manufacturing lets you match bench sizes, sinks, and storage to the actual space. Lead time conversations are also more real. You can call, you can visit, you can ask what happened. Try doing that easily with a container coming from abroad.
When you Buy Laboratory Furniture for a granulation room, think like the person who will work there at 4 pm on a tiring day, not like a person looking at a catalogue at 10 am. Is there clearance to pull the drum out? A place for cleaned screens so they are not kept “temporarily” on any random surface for three months? Power points away from wet areas? That kind of boring thinking saves hours later.
And when people Buy Laboratory Furniture made locally by TOPTEC Scientific, the other thing they usually want — even if they do not say it on day one — is someone accountable later. A hinge goes, a size needs adjusting, one more cabinet is needed six months later in the exact same finish. Local maker, local problem, local solution. In our market, that is not a small advantage.
If I had to compare two machines tomorrow, this is my list
Not a very fancy list. It is the list I would write on the back of the quotation, honestly.
Real output on my mesh, not their mesh. Whether speed is adjustable. Motor and what power my room actually has. Contact steel, with certificate, not just words. Which screens come with it and where the next screen will come from. How it opens for cleaning — shown, not promised. Emergency stop and interlocks working. Papers. Spare parts and service time in Pakistan. And finally, total cost after the truck, installation, and qualification, not just the pretty machine price.
If the cheaper machine fails on steel, screens, cleaning, and service, it is not cheaper. It is just delaying the payment. With interest.
My final, non-salesy advice
Do not get hypnotised by “300 kg per hour”.
Look at your batch. Look at your formulation. Look at whether the speed can be controlled instead of tolerated, and whether your QA team can clean and defend those contact surfaces without inventing stories. That is the machine you want.
Get it in writing. Test it like you mean it. Involve QA before the advance payment, not after the machine is standing in your facility and everyone is emotionally attached to it.
Whether new or second-hand, a careful buyer in Pakistan will almost always beat a hurried buyer, even if the hurried buyer got a slightly lower price. I have seen that pattern too many times now. Slow down for one day. It can save you months.
And that buyer from the start of this article, with the 200 kg machine that gave him 60? He did not need a bigger machine. He needed a better question before buying. Most of us do.
Questions people actually ask me
“Sir, lab model lena chahiye ya direct production wala?”
If you are still fixing your formulation, lab model. You will waste less and learn faster. Production size looks impressive but teaching it manners on small trial batches gets expensive.
“Speed zyada rakhne se granules behtar bante hain?”
Not necessarily. Sometimes speed zyada and you just produce more fines, faster. Which is not improvement. It is just producing your problem more efficiently.
“316L ka certificate seller na de to?”
Then do not assume it is 316L. Simple. Price should reflect that uncertainty, or you should move to a seller who can document it. In pharma, “trust me” is not a material certificate.
“Second-hand machine ka IQ/OQ/PQ phir se hoga?”
At your site, yes, plan for it. Previous qualification was for a different room, different installation, different everything. Talk to your QA before purchase so the cost and time do not arrive as a surprise gift later.
“Ek hi test material se pata chal jayega machine theek hai?”
Better than no test. Your own material is ideal, but lactose or MCC will still show you screen problems, uneven output, vibration, and a weak drive. An empty machine running quietly proves almost nothing. Remember that.
